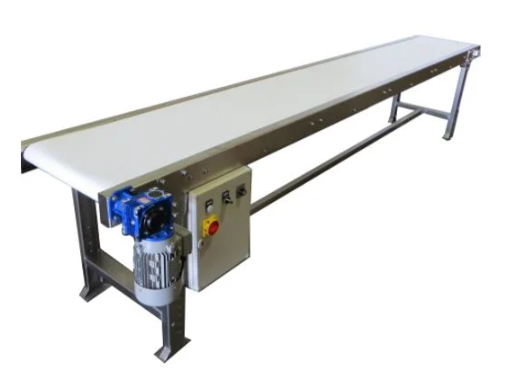
Food processing and food-handling environments require equipment that can meet strict cleanliness and sanitation requirements. Food grade conveyors are designed to move ingredients, packaged foods, and other food-related products efficiently while supporting the hygiene standards required in these facilities.
From food manufacturing plants and commercial kitchens to packaging operations and distribution centers, the right conveyor can help improve material flow while making cleaning and maintenance easier.
What Are Food Grade Conveyors?
Food grade conveyors are conveyor systems designed specifically for environments where food products are handled or processed. Unlike standard industrial conveyors, food grade models are constructed with materials and components that are suitable for food-related applications.
Many food grade conveyors feature stainless steel construction, smooth surfaces, sanitary designs, and components that can withstand frequent cleaning. Depending on the application, conveyors may be used to transport raw ingredients, processed foods, packaged products, or containers through different stages of production.
Common Applications for Food Grade Conveyors
Food grade conveyors can be used throughout a variety of food processing and handling operations, including:
-
Food processing facilities
-
Meat and poultry processing
-
Bakeries
-
Commercial kitchens
-
Beverage production
-
Produce processing
-
Pharmaceutical and food-related manufacturing
-
Packaging and bottling operations
-
Food distribution centers
-
Snack and confectionery production
Conveyors can help move products between workstations, production equipment, packaging areas, and storage locations without requiring employees to manually transport materials.
Stainless Steel Construction
Stainless steel is commonly used in food processing environments because it provides a durable, corrosion-resistant surface that is well suited to regular cleaning.
Stainless steel conveyor frames can also provide a smooth, professional surface with fewer areas where food particles and contaminants can collect. This makes them useful for facilities where sanitation and cleanliness are important considerations.
Easy-to-Clean Conveyor Designs
Sanitation is one of the most important considerations when selecting a conveyor for food applications. Food grade conveyors may incorporate designs that make cleaning and inspection easier.
Features to consider include:
-
Smooth, accessible surfaces
-
Stainless steel frames
-
Washdown-compatible components
-
Sanitary conveyor belts
-
Minimal crevices and collection points
-
Easy-access components for maintenance
-
Corrosion-resistant construction
The appropriate design will depend on the food product, cleaning process, operating environment, and sanitation requirements of the facility.
Choosing the Right Food Grade Conveyor
Not every food-handling operation has the same conveyor requirements. Before selecting a conveyor, consider the type of product being transported and how the conveyor will be cleaned.
Important factors include conveyor size, belt material, load capacity, conveyor speed, construction materials, and the type of cleaning required.
You should also consider whether the conveyor will transport loose food products, ingredients, containers, or packaged goods. Products with different shapes, weights, temperatures, and textures may require different conveyor configurations.
Improve Food Processing Workflow
A properly designed conveyor system can help create a more efficient workflow by keeping products moving between different stages of an operation.
Instead of employees repeatedly carrying products or ingredients from one location to another, conveyors can provide a consistent path through the facility. This can help reduce unnecessary handling and create a more organized production process.
Food grade conveyors can be incorporated into larger material handling systems alongside workstations, packaging equipment, shelving, racks, and other food processing equipment.
Find Food Grade Conveyors at A Plus Warehouse
Whether you're moving ingredients through a production line or transporting finished products toward packaging and distribution, food grade conveyors can provide an efficient solution for food-handling environments.
When selecting a conveyor, consider the product being moved, required capacity, available space, cleaning procedures, and operating conditions to find the right system for your application.
Shop food grade conveyors and other material handling equipment at A Plus Warehouse to help improve the efficiency and organization of your food processing or handling operation.
Check out our food grade conveyor!